
Laser-cut, flame-polished and sanded acrylic edges compared
Updated Oct 2026TL;DR: A CO2 laser leaves cast acrylic with a glossy, almost glass-like edge, which is the finish most people try to get with a torch. You rarely need to change it. Choose a frosted edge (several low-power passes) for a satin look, a sanded edge for flat glue joints and stacked layers, and flame polishing or buffing for saw-cut or CNC-cut edges. Extruded acrylic cuts with a softer, sometimes hazy edge and is more prone to cracking near the cut.
What a laser-cut edge actually is
A CO2 laser does not saw acrylic. It vaporises a narrow slot, and the walls of that slot melt for a moment and re-solidify. On cast acrylic, that thin melted skin cools smooth and glossy. That is why a well-tuned laser cut looks flame-polished straight off the bed.
Two things shape that edge:
- Taper. The beam is a narrow cone, focused to its tightest point at one height. Away from that point it is slightly wider, so the edge has a small slope from top to bottom. On 3 mm it is subtle. On 6 mm and thicker you can see it. See laser cutting 101 for the beam geometry.
- Material. Cast and extruded acrylic melt differently, so they leave different edges. More on that below.

The five finishes side by side
| Finish | Look | Effort | Tools | Best for | Watch out for |
|---|---|---|---|---|---|
| Laser-cut cast | Glossy, clear, slight taper | None | Laser | Ornaments, signs, earrings, most projects | Haze if the lens is dirty or the cut is too fast |
| Laser-cut extruded | Glossy but softer, can look hazy | None | Laser | Hidden edges, outline-only display parts | Stress cracks near the edge, especially with solvents |
| Frosted multi-pass | Satin, even, light-diffusing | Low | Laser | Glowing outlines, matte modern pieces | Needs a test to dial in passes |
| Sanded | Matte, flat, square corners | Medium | Sanding block, wet-and-dry paper | Glue joints, stacked layers, flush fits | Rounded corners if you rock the block |
| Flame polished | Very glossy, rounded corners | Medium | Small torch | Saw-cut and CNC-cut edges | Bubbles, warping, crazing, fire |
Laser-cut cast acrylic: the default
For most laser crafters, the as-cut edge on cast acrylic is the finished edge. No sanding, no torch. If yours looks hazy, frosted or sooty instead of glossy, the cause is almost always one of five things: a dirty lens, focus, speed, masking or air assist. The checklist in how to laser cut cast acrylic cleanly walks through each one.
Two practical tips for the cleanest edge:
- Lower air assist slightly on the final cut. Strong air cools the melted skin faster, which reduces the polished look.
- One slow pass beats two fast ones. A second pass re-melts the edge unevenly and can leave a visible line.
Laser-cut extruded acrylic
Extruded acrylic has a lower molecular weight and more internal stress than cast. It melts more and vaporises less cleanly, so the edge is softer and can look hazy or show drag marks. The bigger concern is stress. Extruded edges are more likely to develop fine cracks (crazing) later, especially if they come into contact with solvent cement, alcohol or a cleaner that attacks acrylic.
Most of the acrylic we stock is cast. A few types, such as some mirror colours, are extruded, and each listing says which. For the full comparison, see cast vs extruded acrylic for laser cutting.
Frosted edge: several low-power passes
If you want a satin edge instead of a glossy one, you can get it on the laser. Instead of one full-power pass, cut with several passes at lower power. Each pass removes material without building up the melted skin that turns glossy, so the edge comes out evenly frosted.
There is no universal recipe. Start with half your normal power, the same speed, and add passes until the part drops out. Note the result and adjust. Frosted edges scatter light, so on a lit piece they glow softly instead of looking clear. They also match the look of a frosted engraving on the face.
Sanded edge: flat, matte and good for gluing
Sanding is the way to get a perfectly flat, square edge. It removes the laser taper and gives a uniform matte finish.
- Clamp the part or hold it flat on the bench.
- Wrap wet-and-dry sandpaper around a flat block. Start at 220 or 240 grit if you need to remove taper, or 400 if you only want a matte finish.
- Sand along the edge with the block flat against it. Do not rock it, or the corners round over.
- Work up through the grits: 400, then 600. Stop here for an even matte edge.
- Keep the paper wet. Water keeps the acrylic cool and the paper from clogging.
A sanded edge is the best surface for gluing edge to face or stacking layers flush. It is flat, so the joint closes fully, and the fine texture gives adhesive something to grip. See best glues for acrylic for which adhesive to use.
To go from sanded to clear, keep going: 800, 1000, 1500 and 2000 grit wet, then a plastic polish on a soft cloth or a buffing wheel. It takes time, but it gives a clear edge without a torch.
Flame polishing: for saw and CNC edges
Flame polishing melts the very surface of an edge with a small torch so it flows smooth and glossy. It is the standard finish for acrylic cut with a saw or router, which leaves tool marks. After a laser, it is rarely needed, because the laser has already done the same job.
If you do flame polish:
- Remove the protective film first. Film burns and leaves residue on the face.
- Sand the edge smooth first. A flame polishes a surface; it does not remove saw marks.
- Use a small, hot, blue flame and pass it along the edge at a steady speed. Do not stop in one place.
- Bubbles mean too slow or too close. Speed up. Bubbles cannot be fixed without sanding back.
- Thin parts warp. On 1.5 mm and small pieces, the heat spreads into the part. Sand and buff thin parts instead.
Acrylic is flammable. Flame polish on a clear, non-flammable surface, away from offcuts and paper, with a fire extinguisher in reach. Never flame polish inside or near your laser.
Flame-polished edges hold some internal stress. Solvent cement or alcohol near a flame-polished edge can craze it, sometimes days later. If the part will be glued, glue first, or use a sanded and buffed edge instead.
Edges on two-tone, mirror and glitter acrylic
Layered and speciality sheets show their construction in the edge, whatever the finish:
- Two-tone and three-tone engravable acrylic shows a stripe of the core colour along the edge. A laser cut keeps it neat. Sanding or flame polishing does not hide it.
- Mirror acrylic shows the painted backing as a thin dark line at the back of the edge.
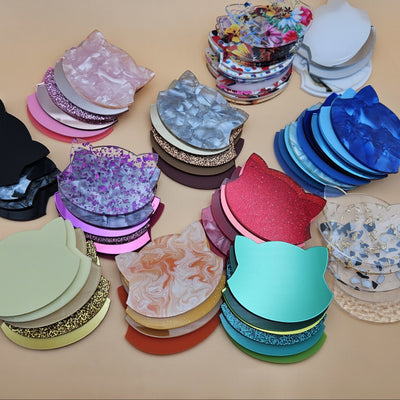
- Glitter acrylic sparkles in the edge, because the glitter runs through the whole sheet.

For more on these materials, see mirror, glitter and coloured acrylic and our two-tone engravable acrylic.
Which finish for which project
- Ornaments, earrings, keychains, cake toppers: laser-cut cast, as it comes off the bed.
- Signs and nameplates: laser-cut cast. Sand only if the sign sits in a slot or frame that needs a flat edge.
- Edge-lit signs: laser-cut cast for the visible edges. The bottom edge sits on the LED base; sanding it flat helps it sit square and take in light evenly.
- Stacked layered art: laser-cut cast. Sand edges that must sit flush against another part.
- Boxes and glued assemblies: sand the mating edges for flat, strong joints.
- Saw-cut or score-and-snap edges: sand, then flame polish or buff if the edge will show. See how to cut acrylic without a laser.
Frequently asked questions
Q: Do I need to flame polish laser-cut acrylic? A: Usually not. A CO2 laser leaves cast acrylic with a glossy edge that already looks flame-polished. Flame polishing is for saw-cut and CNC-cut edges.
Q: Why is my laser-cut acrylic edge frosted instead of clear? A: On cast acrylic, the usual causes are a dirty lens, focus set wrong, cutting too fast or too much air assist. If the sheet is extruded, a softer, hazier edge is normal.
Q: How do I get a frosted edge on purpose? A: Cut with several low-power passes instead of one full-power pass. Test on an offcut to find the number of passes for your laser.
Q: What grit should I sand acrylic edges with? A: Start at 220 or 240 to remove taper, then 400 and 600 for an even matte finish. Continue to 2000 and polish if you want a clear edge.
Q: Can I flame polish acrylic with a lighter? A: No. A lighter flame is too cool and sooty and tends to leave a smoky, uneven finish. Use a small torch with a hot blue flame, or sand and buff instead.
Q: Why did my acrylic crack after I glued it? A: Solvent cement can craze stressed edges, especially extruded acrylic and flame-polished edges. Use cast acrylic, a laser-cut or sanded edge, and the right adhesive for the joint.